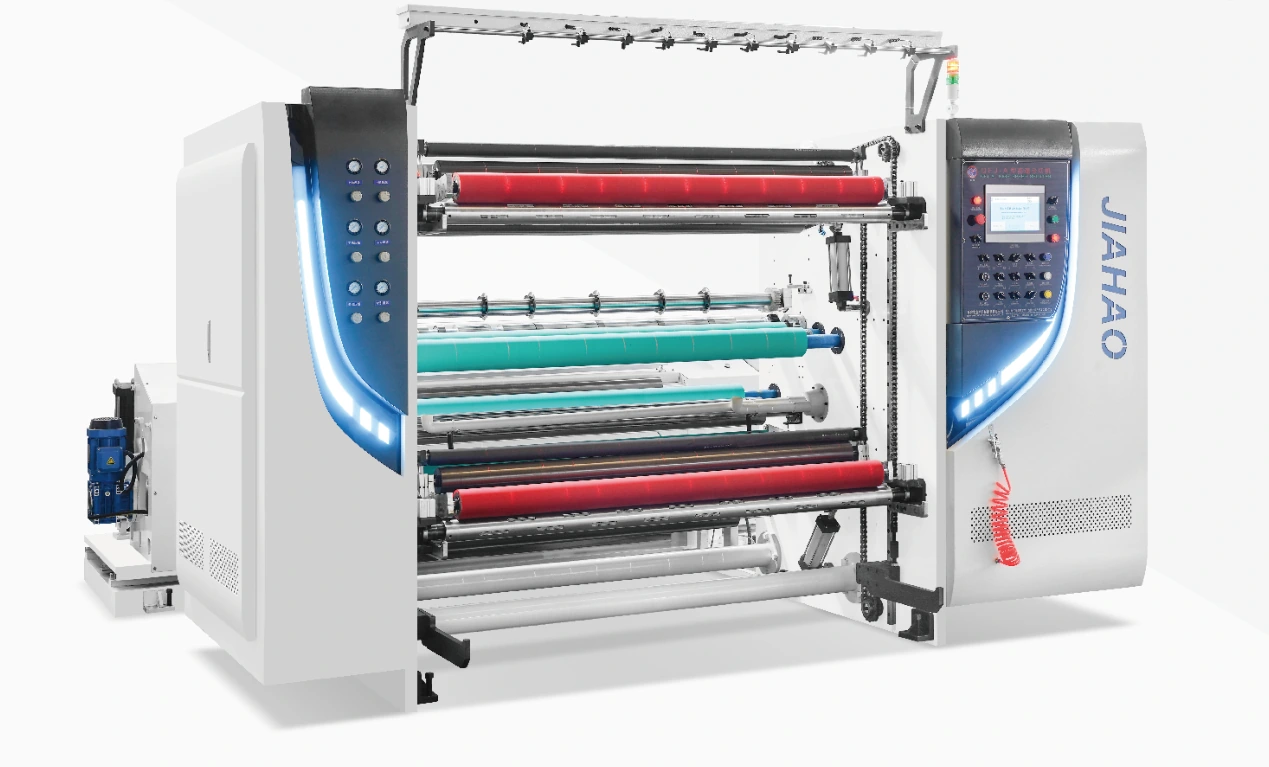
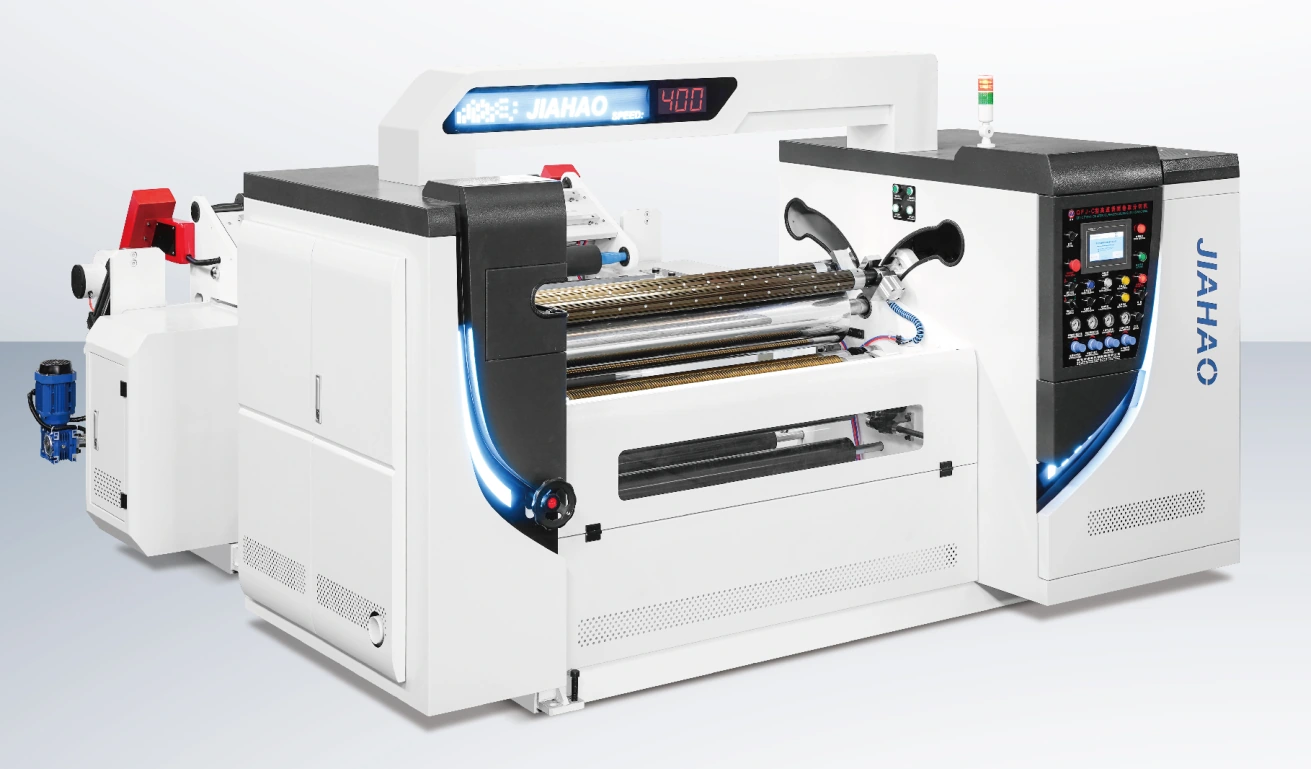
Ground-Roll Winding Layout
The machine uses a ground-roll arrangement for large-diameter winding. Review how the roll is supported, driven and removed for the intended web and finished-roll mass.

SLITTING & REWINDING · QFJ-LM400
Convert larger rolls with a ground-roll winding layout. The LM400 lists 400 m/min, a 1,500 mm parent-roll diameter and 1,200 mm finished-roll diameter, with 1,600, 2,000 and 3,000 mm working-width configurations.
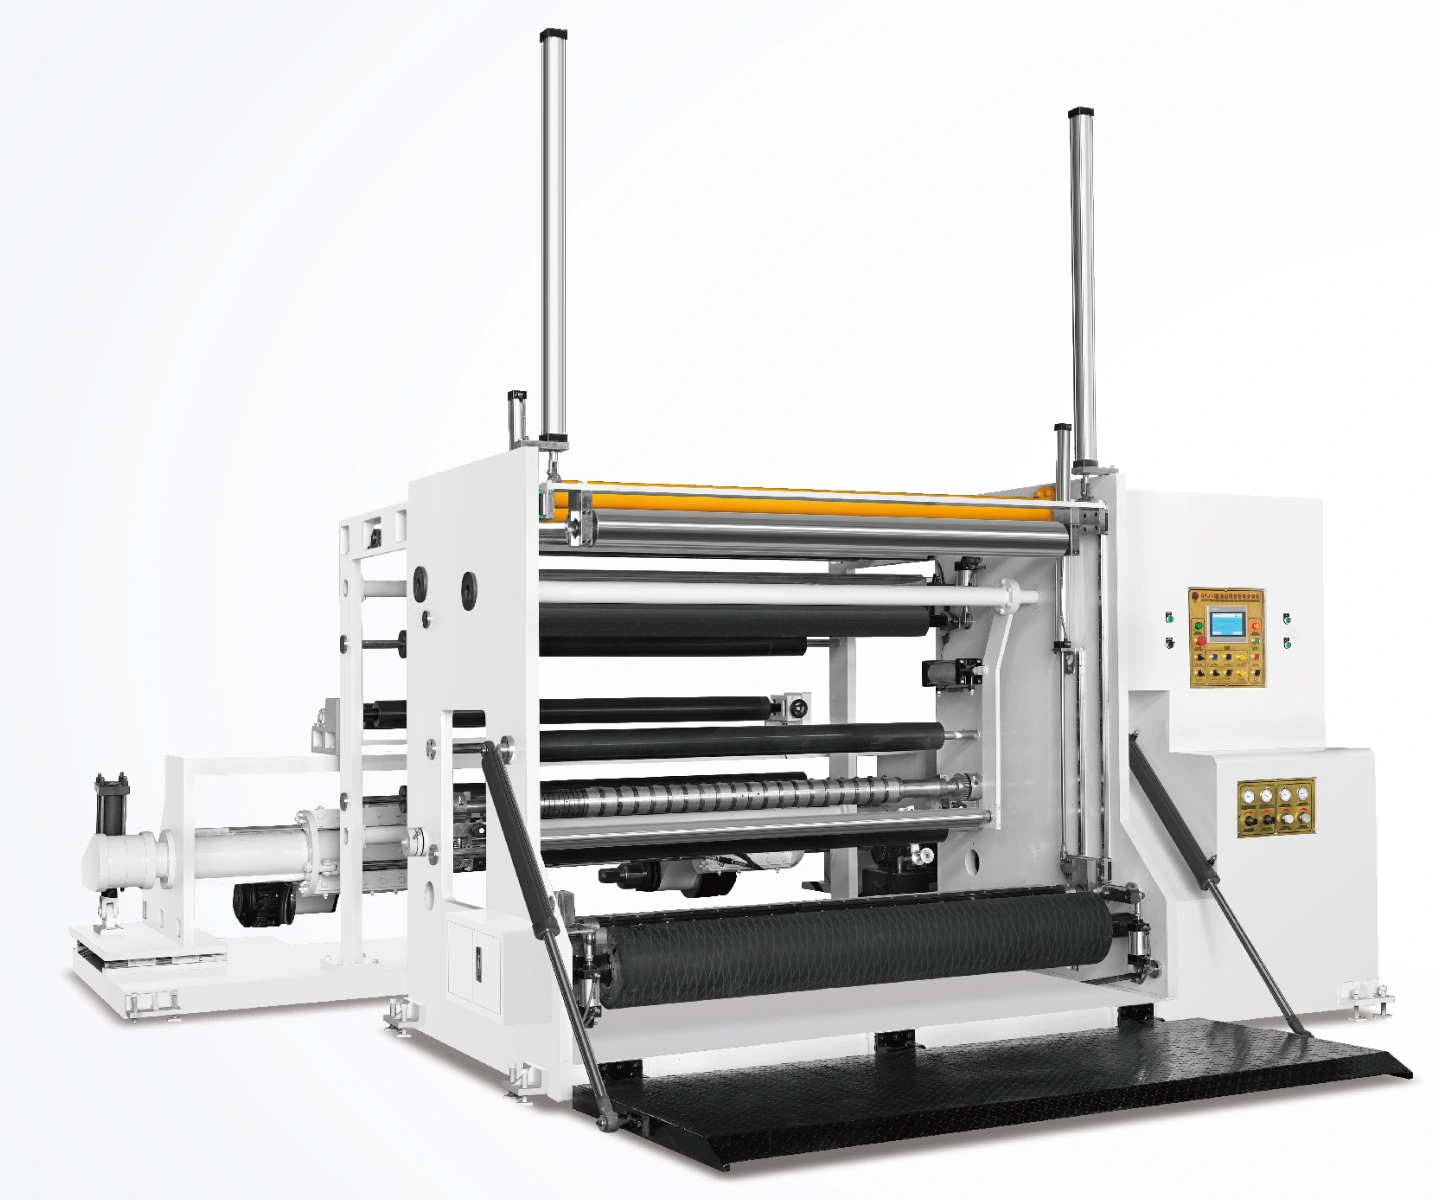
Listed configuration values. Production speed and practical slit pattern depend on the material and the agreed machine setup.
Consider LM400 when large finished rolls and wider webs determine the machine choice. Its 100 mm minimum slit makes it a different starting point from narrow-lane differential-shaft models. Include roll mass, floor loading, loading access and the removal route in the layout review.
CONSTRUCTION & CONTROL
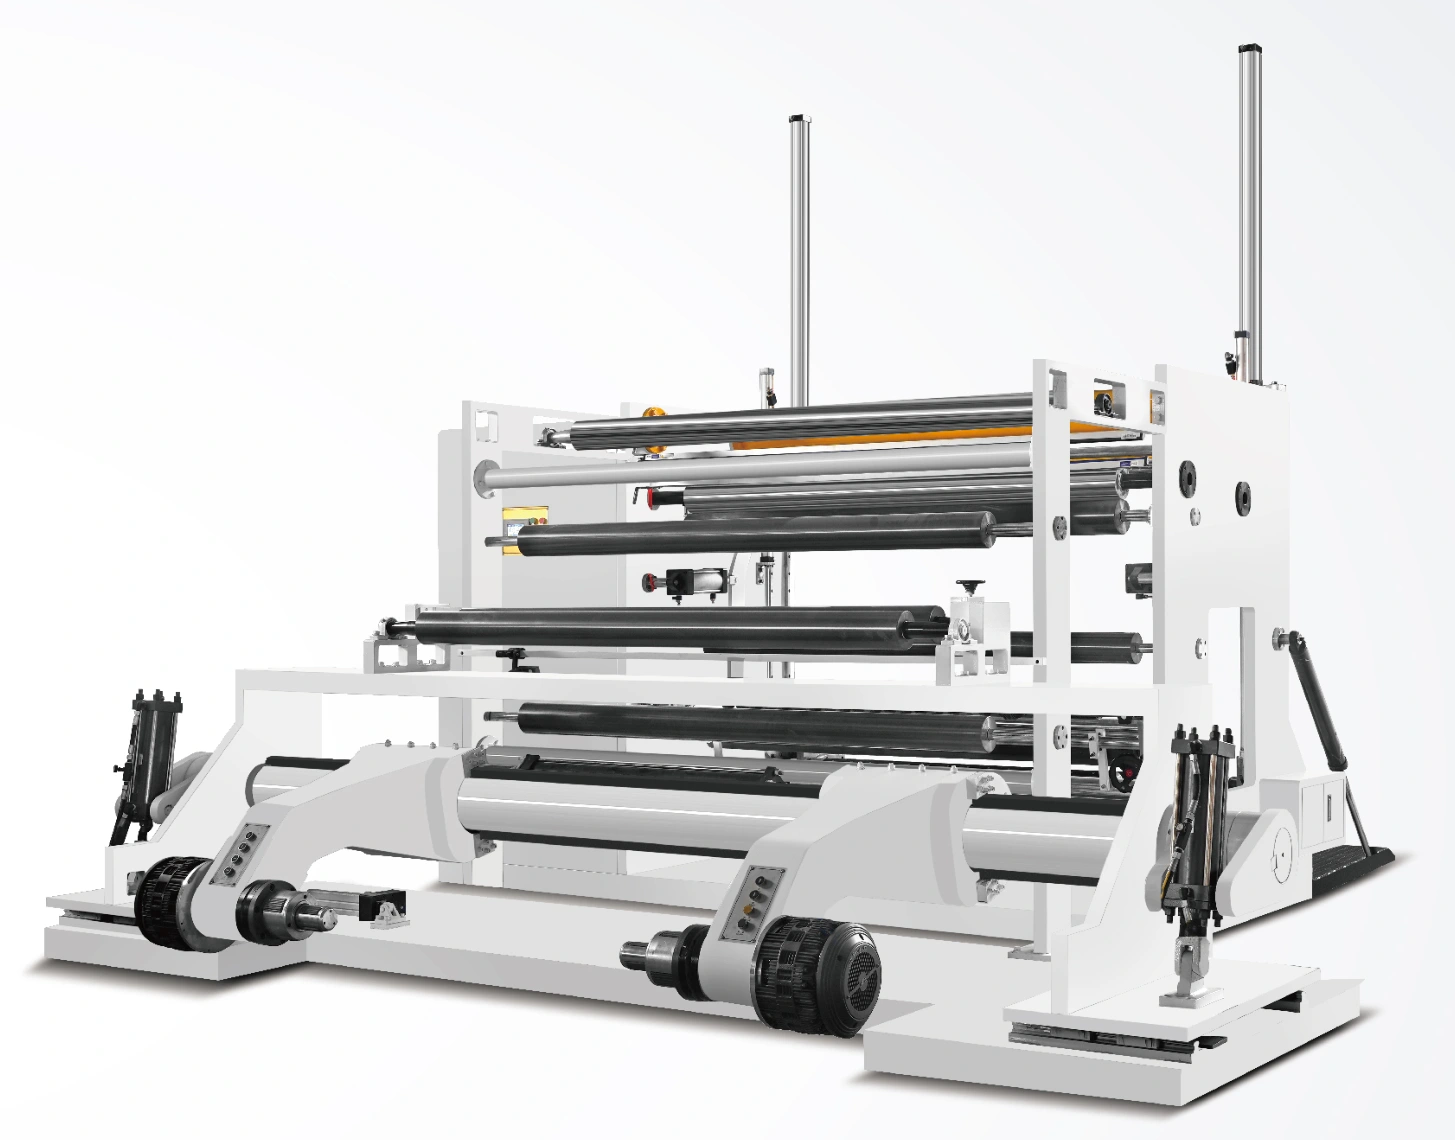
The machine uses a ground-roll arrangement for large-diameter winding. Review how the roll is supported, driven and removed for the intended web and finished-roll mass.
Shafted and shaftless winding arrangements are described for this format. Specify the required core interface and handling sequence so the proposal identifies the arrangement being supplied.
Four sets of servo control are listed. Drive entries vary with working width; the motor table is a configuration reference rather than a total connected-load figure.
The parent and finished diameters are 1,500 and 1,200 mm respectively. Weight limits, lifting equipment and floor requirements need a matching layout and loading specification.
MATERIAL & FINISHED ROLL
Provide the paper grade, grammage, coating and target roll structure. Include edge dust and roll firmness among the checks relevant to the next converting stage.
PVC, BOPP, CPP, PET and composite films require review by thickness, stretch and surface sensitivity. Confirm the contact and winding conditions for the actual construction.
Specify foil grade, thickness and temper. Agree the acceptable slit edge and roll appearance with representative material and a defined lane pattern.
WIDTH & DRIVE CONFIGURATIONS
| Parameter | 1600 configuration | 2000 configuration | 3000 configuration |
|---|---|---|---|
| Unwinding width | 1,600 mm | 2,000 mm | 3,000 mm |
| Listed slitting speed | 400 m/min | 400 m/min | 400 m/min |
| Minimum slit width | 100 mm | 100 mm | 100 mm |
| Parent-roll diameter | 1,500 mm | 1,500 mm | 1,500 mm |
| Finished-roll diameter | 1,200 mm | 1,200 mm | 1,200 mm |
| Main servo power | 2 × 11 kW | 2 × 16 kW | 2 × 22 kW |
| Circular-knife motor power | 2.2 kW | 2.2 kW | 2.2 kW |
| Unwinding servo power | 7.5 kW | 2 × 7.5 kW | 2 × 11 kW |
Listed values describe the configuration shown. Confirm working width, roll mass, core interfaces, voltage, frequency and the complete supplied scope in the proposal. Production conditions and acceptance criteria depend on the actual material. Motor entries are individual ratings, not total installed electrical load. The 2.2 kW row describes circular-knife power.
SETUP, OPERATION & ACCEPTANCE
Record parent and finished width, diameter, mass and core separately. Check lane widths against the 100 mm listed minimum.
Review handling equipment, floor loading, clearances and operator positions on the proposed layout.
Confirm knife setup, web guidance, tension and contact conditions for the chosen material and working width.
Assess slit width, edge condition, firmness and downstream unwind behaviour throughout the roll build.
Review the floor plan, service clearance, roll-handling route and utilities before installation. Agree commissioning and operator-training requirements with the proposal. Keep the machine identification, shaft interfaces and blade dimensions available for maintenance and spare-part inquiries.
Compare AF400 for a 1,200 mm parent and 1,000 mm finished-roll envelope. A500 is a differential-shaft alternative for narrower lanes and smaller finished rolls. Match roll size, winding principle and slit pattern before comparing headline speeds.
BEFORE YOU SPECIFY
No. Diameter and mass are separate requirements. Confirm weight capacity, core interfaces and handling equipment for the proposed configuration.
The listed minimum slit width is 100 mm. Review narrower-lane needs against other configurations rather than assuming the same knife and winding arrangement.
They are alternative arrangements to specify. The quotation and layout should identify which construction and handling equipment are included.
It is listed as circular-knife power in the Chinese parameter row. It is not a total electrical load or a finished-roll capacity.
MATERIAL & PRODUCTION REQUIREMENTS
Compare material requirements and winding formats before defining the final machine configuration.
QUOTATION & SUPPLY SCOPE
Request a QFJ-LM400 quotation against your material, working width and finished-roll targets. Identify the selected version, cutting and winding arrangement, loading equipment and controls in the proposed supply.
Ask for standard equipment and optional items to be listed separately. Include commissioning, operator training, documentation and initial spare-part requirements in the discussion.
Provide quantity and destination. Confirm price, currency, delivery basis, packing, production schedule and any excluded freight or import charges in the quotation.
Agree representative material inspection, measurement criteria and supplied configuration before ordering. Confirm warranty terms, installation responsibilities and spare-part support with the proposal.
COMPARE MACHINE FORMATS
YOUR MATERIAL. YOUR FINISHED ROLL.
Share the web construction, incoming roll, slit pattern and finished-roll requirements. Include the information you already have.